Specifying AR coated glass for security and surveillance cameras is largely a matter of deciding which three numbers actually govern the application and letting the rest follow. This guide walks through the parameters that belong on the drawing, the tolerances that genuinely change the price, and the specification items that are routinely left out and then argued about at first article.
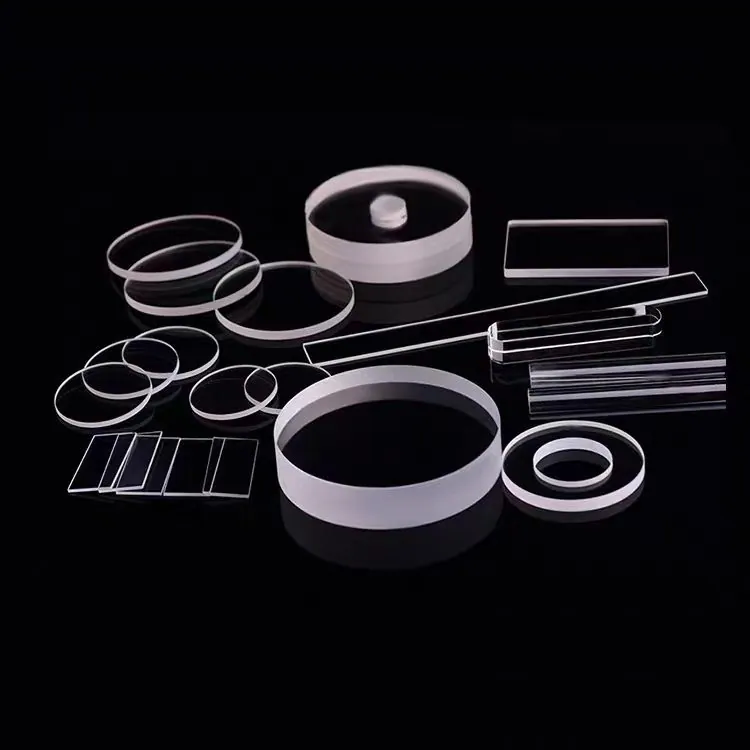
AR Anti-Reflective Glass in Security and Surveillance Cameras
In security and surveillance cameras, that translates into a specific set of requirements rather than a general preference for quality. Surveillance cameras run continuously, often outdoors, and must deliver usable images at night under near-infrared illumination. That combination makes IR-cut behavior and window durability the two defining requirements: the window has to pass the day spectrum faithfully, block infrared during daylight, and still transmit 850 nanometer illumination after dark on dual-mode designs.
How AR coated glass works in practice
An anti-reflective coating reduces the light that bounces off a glass surface instead of passing through it. Uncoated optical glass reflects roughly four percent per surface, which means a two-sided window can lose almost eight percent of the light and, worse for a display or a camera, that reflected light comes back as glare and ghost images. A single-layer magnesium fluoride coating reduces each surface to about one and a half percent, and a multilayer broadband design brings it under half a percent across the visible band. The result is both more transmitted light and a much darker, more neutral residual reflection. In Security and Surveillance Cameras, that combination is what turns a piece of glass into a window that appears to disappear - the visual signature of a properly coated part is that the viewer notices the object behind it rather than the glass itself.
The tolerances that actually matter
AR specifications are photometric rather than dimensional. The useful numbers are average reflectance across a stated band, maximum reflectance at the worst wavelength, transmission, haze, and the residual color of the reflection. Average reflectance below 0.5 percent per surface is a normal industrial specification, and below 0.2 percent is achievable with more layers; haze should stay under 0.3 percent, and ideally under 0.1 percent, because haze is what an observer perceives as a gray film. Dimensional tolerances - outline, thickness, chamfer and edge quality - follow the housing. In Security and Surveillance Cameras, the specification item most often missed is the color of the residual reflection: a coating that meets every photometric target can still read visibly blue or green, and for a display or an architectural window that color is the first thing a customer sees.
Design rules that reduce cost
Deciding what to coat is as important as deciding how. Coat both faces whenever possible, because the second surface typically contributes as much reflected light as the first. Choose the band from the light source rather than from habit: a visible-only coating on a sensor window that also passes 850 nm illumination will reflect that illumination back into the system. Keep a clear margin of 0.5 to 1 mm around the aperture for adhesive or gaskets, and specify chamfers so that handling never touches a coated face. Where a display is laminated, confirm that the optical adhesive's index matches the coating design, since a mismatch reintroduces a reflection at an internal interface. In Security and Surveillance Cameras, these details are what separate a part that looks invisible from one that merely measures well.
Coating and deposition considerations
AR stacks are built from alternating low-index silica and higher-index oxides such as niobium, tantalum or titanium oxide, deposited in four, six or more layers to flatten the reflectance curve across the band. Broader bands and lower reflectance both require more layers, and more layers mean tighter process control, because each layer contributes to the interference balance. Ion-assisted deposition is preferred for durability: the resulting films are dense, so they resist moisture, resist abrasion and do not shift color when humidity changes. Hydrophobic and oleophobic top layers are frequently added on touch surfaces, and a conductive or anti-static layer helps where dust retention is a problem. For Security and Surveillance Cameras, the deposition process also determines whether the coating can be applied to both faces in one run or needs two passes.
Inspection and measurement
The primary measurement is spectral reflectance and transmission across the specified band, ideally at several points across the aperture so that thickness uniformity is verified as well as average performance. Haze is measured on a haze meter and matters more than most specifications acknowledge: a coating with excellent reflectance and 1 percent haze will be rejected by the user, because haze is visible at almost any viewing angle. Durability is verified through abrasion, tape adhesion and humidity tests, often against MIL-C-48497 or an equivalent customer standard. In Security and Surveillance Cameras, the incoming inspection that pays for itself is a simple reflection color check under a defined light source, which catches color casts before the glass is bonded into an assembly that cannot be reworked.
Requirements specific to Security and Surveillance Cameras
In security and surveillance cameras, that translates into a specific set of requirements rather than a general preference for quality. Surveillance cameras run continuously, often outdoors, and must deliver usable images at night under near-infrared illumination. That combination makes IR-cut behavior and window durability the two defining requirements: the window has to pass the day spectrum faithfully, block infrared during daylight, and still transmit 850 nanometer illumination after dark on dual-mode designs.
- IR-cut edge between 645 and 680 nm
- Outdoor-grade abrasion and salt spray resistance
- Hydrophobic topcoat for rain shedding
- Service life of five years or more with no transmission loss
IP-rated enclosure compatibility, MIL-style abrasion and humidity testing, RoHS and REACH declarations, and increasingly NDAA-related supply chain documentation.
Selection data at a glance
| Parameter | Typical value | Notes |
|---|---|---|
| Reflectance per surface | R ≤ 0.5 % average, R ≤ 0.2 % achievable | 420-680 nm |
| Transmission gain | up to 99 % single side, > 99 % both sides | Versus 92 % uncoated B270 |
| Band options | 400-700, 400-1100, 900-1700 nm, dual band | Broadband or tuned |
| Substrate | B270, ultra-clear, borosilicate, quartz, acrylic | 0.5-12 mm |
| Haze | ≤ 0.3 %, typically ≤ 0.1 % | Haze meter |
| Abrasion | pencil hardness 9H, steel wool 0000 pass | Hard oxide stacks |
| Adhesion | tape test 4B or better | Cross-hatch |
| Environmental | 85/85 humidity, salt spray, UV stable | Outdoor grades available |
| Coating pattern | full face, aperture only, or masked | Margin 0.5-1 mm typical |
Frequently asked questions
Why does the reflection look blue or green?
Because the stack balances reflectance across the band rather than at every wavelength identically. The residual color can be tuned to neutral, but doing so usually requires more layers, so specify the acceptable residual color explicitly.
Do you offer anti-glare as well as anti-reflective treatment?
Yes. Anti-reflective coating maximises transmitted light while anti-glare etching scatters reflected light for readability. Many display products combine a coated front face with an etched surface where the customer wants both.
What reflectance can an AR coating actually reach?
Under 0.5 percent average per surface is routine, and under 0.2 percent is achievable across the visible band with a multilayer stack. Total transmission above 99 percent is possible when both faces are coated.
Need a quotation for ar anti-reflective glass?
Send your drawing, target specification or coating requirement and an optical engineer will reply within 24 hours with a price and a lead time.
Request a Quote Email an engineer