A part that measures correctly in the lab and fails in service is almost always a qualification gap rather than a manufacturing defect. This article sets out how quartz and crystal glass is inspected and qualified for biometric and fingerprint recognition, which standards apply, which tests reveal real weaknesses, and what documentation should travel with a shipment.
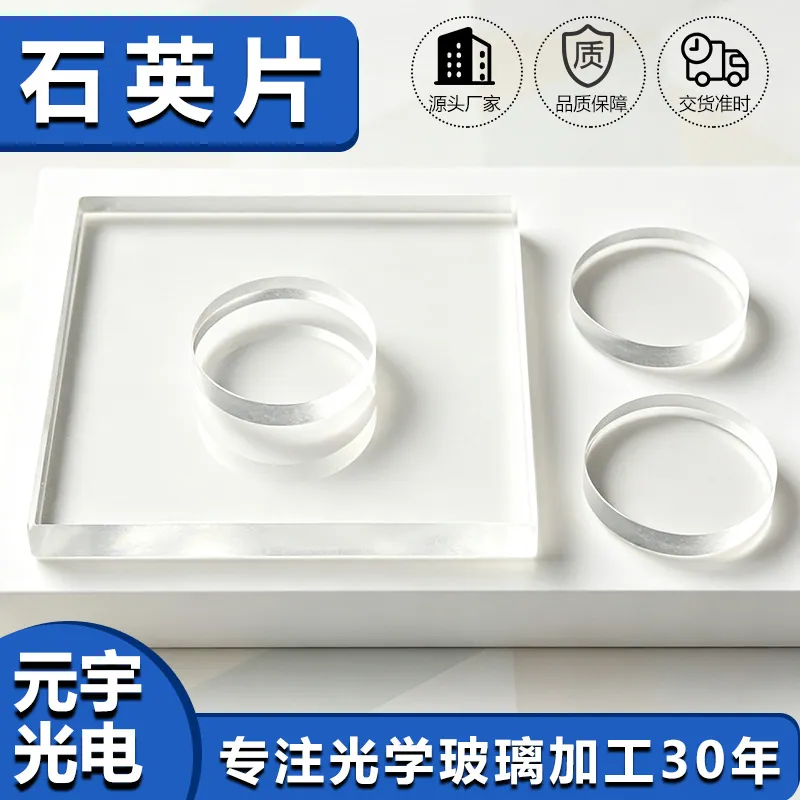
Optical Quartz and Crystal Glass in Biometric and Fingerprint Recognition
In biometric and fingerprint recognition, that translates into a specific set of requirements rather than a general preference for quality. Biometric systems must separate the live signal from everything else in the scene, which makes spectral filtering the primary function of the optics. Fingerprint and iris systems work at defined wavelengths, often under near-infrared illumination, and a filter that leaks the wrong band will compromise recognition as surely as a dirty sensor.
Common failure modes and how they show up
Quartz failures tend to be optical or thermal rather than mechanical. Solarisation, a gradual loss of UV transmission under prolonged exposure, occurs in some grades and is prevented by choosing high-OH material. Devitrification, the conversion of the amorphous surface into crystalline form at high temperature in the presence of contamination, produces a permanently hazy surface and is usually caused by alkali or metal contamination during handling or firing. Thermal stress cracks appear where a part is clamped or where an unaccounted gradient exists. Coating absorption causes damage spots in laser service. In Biometric and Fingerprint Recognition, a failure that appears at high temperature should always prompt a review of what touched the part - handling gloves, marking pens and packaging are all common sources of the contamination that triggers devitrification.
Handling, cleaning and packaging
Quartz is hard but brittle, and its fine edges chip easily, so the handling rules are stricter than for soda-lime. Ground and chamfered edges are normal, and parts are usually supplied interleaved with a particle-free separator. Cleaning avoids hydrofluoric-acid-containing products entirely, since even trace HF attacks silica, and it avoids strong alkaline solutions that can etch the surface over time. Fingerprints on a UV part are functional defects, not cosmetic ones, because organic residue absorbs strongly below 250 nm and will be burned into the coating by UV exposure. In Biometric and Fingerprint Recognition, the packaging standard matters as much as the part: a scratch introduced in transit on a deep-UV window can be undetectable on arrival and fatal in service.
Inspection and measurement
Inspection of quartz parts extends beyond the usual surface quality checks. Transmission should be measured across the band of interest, including the deep UV where an ordinary spectrophotometer may not reach. Homogeneity and birefringence are checked interferometrically or with a polariscope, and inclusions are assessed against a bubble class. For laser optics, laser-induced damage threshold testing on a witness sample from the same lot gives far more confidence than a certificate alone. Dimensional checks follow the drawing, with particular attention to wafer TTV. In Biometric and Fingerprint Recognition, a witnessed damage test is often the only way to justify a material change to an internal customer, because the performance difference between two quartz grades may not be visible in any other measurement.
Standards, documentation and traceability
Quartz optics are specified through the same drawing standards as other elements, ISO 10110 and ISO 12123, with additional material specifications covering OH content, bubble class and homogeneity. Laser applications reference damage threshold test standards and often require witness-sample data. Cleanliness specifications become important for semiconductor-adjacent parts, where particle count per unit area is controlled and documented. Environmental compliance is covered by RoHS and REACH declarations. In Biometric and Fingerprint Recognition, the documentation that most often determines whether a part can be released is traceability back to the material lot, because a homogeneity or inclusion problem discovered during assembly can only be contained if the affected parts can be identified.
Substrate and material selection
Within fused silica there is a real choice to make. Low-OH grades have almost no hydroxyl content and transmit further into the infrared, with less absorption around 2.7 micrometers, so they suit IR and high-power applications. High-OH grades contain several hundred parts per million of hydroxyl and are preferred where deep UV performance and resistance to solarisation matter. Natural quartz is used where its crystalline properties are needed, but it carries more inclusions and its anisotropy complicates polishing. Synthetic crystal (cultured quartz) offers the same optical behavior with better consistency. In Biometric and Fingerprint Recognition, the specification that prevents most disputes is not a grade name but a set of numbers: OH content, bubble class, and the transmission curve over the band of interest.
Requirements specific to Biometric and Fingerprint Recognition
In biometric and fingerprint recognition, that translates into a specific set of requirements rather than a general preference for quality. Biometric systems must separate the live signal from everything else in the scene, which makes spectral filtering the primary function of the optics. Fingerprint and iris systems work at defined wavelengths, often under near-infrared illumination, and a filter that leaks the wrong band will compromise recognition as surely as a dirty sensor.
- Tight band-pass or IR-cut definition at the operating wavelength
- Scratch-resistant user-facing surface
- Stable behavior across a wide angle of incidence
- High transmission for low-power illumination
ISO/IEC 19794 context for biometric data quality, ISO 10110 drawings, and RoHS and REACH declarations.
Selection data at a glance
| Parameter | Typical value | Notes |
|---|---|---|
| Transmission band | 185-2500 nm (fused silica) | Deep UV to near IR |
| Refractive index | 1.458 (fused silica) | Low and highly uniform |
| CTE | 0.55 × 10⁻⁶ /K | Thermal shock resistant |
| OH content | < 10 ppm low-OH, > 200 ppm high-OH | Selected by UV or IR use |
| Birefringence | < 5 nm/cm (fused) | Crystalline quartz is anisotropic by nature |
| Flatness | λ/4 to λ/10 | Quartz wafers to λ/20 |
| Scratch-dig | 40-20 standard, 20-10 precision | ISO 10110-7 |
| Thickness range | 0.1-30 mm | Wafers from 0.1 mm |
| Edge finish | ground, chamfered or fine-lapped | Chips ≤ 0.05 mm |
Frequently asked questions
When should I choose quartz rather than optical glass?
When the part must transmit below roughly 300 nm, survive a rapid thermal cycle, or withstand high laser energy. For visible-light windows and filters, borosilicate or B270 performs the same function at a fraction of the cost.
What is the difference between low-OH and high-OH fused silica?
Low-OH material has minimal hydroxyl content and transmits further into the infrared. High-OH material contains several hundred parts per million of hydroxyl, which improves deep-UV transmission and resistance to solarisation.
Why did my quartz window become hazy at high temperature?
That is devitrification, and it is almost always caused by contamination - alkali or metal traces from handling, marking or packaging - rather than by the material itself. Specify contamination-free handling for parts destined for high-temperature service.
Need a quotation for optical quartz and crystal glass?
Send your drawing, target specification or coating requirement and an optical engineer will reply within 24 hours with a price and a lead time.
Request a Quote Email an engineer