A part that measures correctly in the lab and fails in service is almost always a qualification gap rather than a manufacturing defect. This article sets out how IR filters is inspected and qualified for robotics and factory automation, which standards apply, which tests reveal real weaknesses, and what documentation should travel with a shipment.
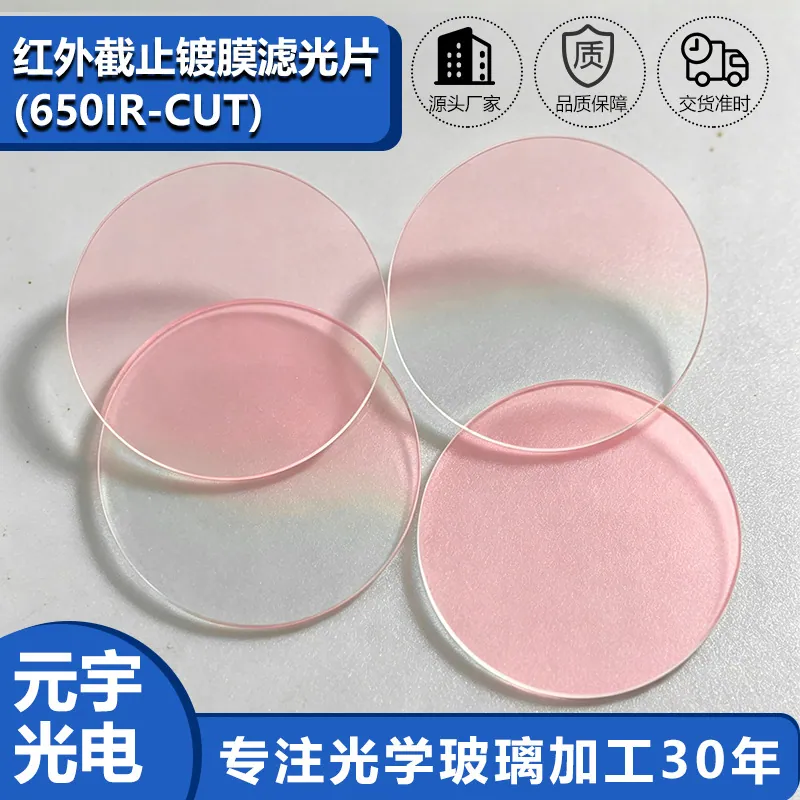
IR Filters in Robotics and Factory Automation
In robotics and factory automation, that translates into a specific set of requirements rather than a general preference for quality. Robots and automated cells use optical components continuously in environments built for metal, not glass: coolant, swarf, vibration and cleaning chemicals. Sensors and vision windows must survive being wiped, bumped and hosed down, while maintaining the repeatability the control system assumes.
Handling, cleaning and packaging
The dichroic surface is both the optical function and the most vulnerable part of the component. Handle by the edge, never wipe dry, and clean only with the approved process: neutral detergent, cascaded deionised water rinses, then an alcohol or nitrogen dry. Fingerprints etch a hard oxide layer over time and create a permanent localised transmission dip that cannot be polished out. Storage uses particle-free interleaves and never stacks two coated faces together. Because the coating is a stack of thin layers, it is also sensitive to mechanical impact at the edge, so a chamfer is standard. In Robotics and Factory Automation, the assembly process deserves equal attention: adhesives that outgas, or a potting compound that cures with shrinkage, can both shift the spectrum of a well-made part.
Inspection and measurement
Spectral measurement is the primary inspection for an IR filter. A spectrophotometer covering 350 to 1100 nm will confirm cut-on wavelength, average visible transmission and blocking depth, and it should be measured at the specified angle - a part measured only at normal incidence can pass while failing in service. Beyond the spectrum, a color filter faces the same physical acceptance criteria as any window: surface quality in scratch-dig, edge chips, chamfer condition and cleanliness. Where the part is bonded or potted, a flatness or transmitted wavefront check matters as well. In Robotics and Factory Automation, asking for a measured curve and an adhesion test result with the first article is what prevents a coating chemistry problem from turning into a field return six months later.
Standards, documentation and traceability
IR filters are qualified through a mix of optical, environmental and compliance specifications. Drawings follow ISO 10110 for surface form and imperfections, and mechanical acceptance commonly cites MIL-PRF-13830B scratch-dig. Environmental durability is usually demonstrated with a humidity soak, a salt spray test, an abrasion test and an adhesion tape test, often against MIL-C-48497. Material compliance is documented through RoHS and REACH declarations. In Robotics and Factory Automation, additional requirements frequently arrive from the customer's own standards - automotive temperature ranges, medical cleaning regimes or outdoor UV exposure - and it is worth establishing those at quotation, because a coating that passes a humidity test can still fail a specific cleaning chemical.
Common failure modes and how they show up
Most IR filter failures are spectral drift, edge damage or delamination. Spectral drift after humidity exposure means the coating was deposited without adequate ion assistance; drift after temperature cycling points to a design that ignored the substrate's expansion. Delamination almost always starts at a chamfer or an uncoated margin and spreads inward. Ghosting or flare, which customers often report as a defect, is normally an optical design issue caused by an uncoated second surface reflecting back into the sensor. In Robotics and Factory Automation, reproducible failures should be diagnosed by measuring the part before and after the environmental stress rather than only after, because that single comparison separates a coating problem from an assembly problem in one step.
Requirements specific to Robotics and Factory Automation
In robotics and factory automation, that translates into a specific set of requirements rather than a general preference for quality. Robots and automated cells use optical components continuously in environments built for metal, not glass: coolant, swarf, vibration and cleaning chemicals. Sensors and vision windows must survive being wiped, bumped and hosed down, while maintaining the repeatability the control system assumes.
- Impact and abrasion tolerance for a factory floor
- Repeatable optical performance over millions of cycles
- Solvent and coolant resistance
- Compact outline with simple mounting geometry
ISO 10218 context for robotic safety, ISO 10110 drawings, and customer-specific environmental test protocols.
Selection data at a glance
| Parameter | Typical value | Notes |
|---|---|---|
| IR-cut cut-on | 630-700 nm | Tuned to the sensor response |
| Visible transmission | T ≥ 90 %, R ≤ 1 % | Average 420-620 nm |
| NIR blocking | OD2 - OD4 (1 % - 0.01 %) | 700-1100 nm |
| Edge steepness | 10-30 nm transition | Dichroic designs |
| Angle of incidence | 0-30 deg specified | Passband shifts blue with angle |
| Wavelength tolerance | ± 5 nm standard, ± 2 nm precision | Measured at stated AOI |
| Substrate | B270, D263T, blue glass, sapphire | Absorptive option removes NIR without angle shift |
| Thickness | 0.3-3 mm | 0.55 - 1.1 mm typical for camera windows |
| Environmental | Humidity, salt spray, abrasion tested | MIL-C-48497 / MIL-PRF-13830B |
Frequently asked questions
Do the filters pass humidity and salt spray testing?
Ion-assisted hard oxide coatings do. Every shipment can include humidity, adhesion, abrasion and salt spray results, and the parts are routinely qualified against MIL-style test methods when the application requires it.
Can you supply the filter laminated to a sensor window or a cover glass?
Yes, coating on thin substrates down to 0.3 mm allows direct lamination or bonding. State the adhesive or bonding method at quotation so the coating stress and the assembly thermal cycle can be considered together.
How tight can the wavelength tolerance be?
Plus or minus five nanometers is routine and plus or minus two nanometers is achievable on precision imaging parts. Tighter than that usually requires sorting parts by measurement, which raises cost sharply.
Need a quotation for ir filters?
Send your drawing, target specification or coating requirement and an optical engineer will reply within 24 hours with a price and a lead time.
Request a Quote Email an engineer